Durability
Designed for long-term service in demanding environmental conditions.
Understanding the method
Exothermic welding—also known as thermite welding—joins metallic conductors through a heat-releasing chemical reaction inside a purpose-designed graphite mould. The reaction produces molten metal that flows around the prepared conductors and solidifies into a molecular bond.
Because the finished joint does not depend on mechanical clamping pressure, a correctly executed weld provides dependable electrical continuity, mechanical strength and corrosion resistance for critical earthing and bonding systems.
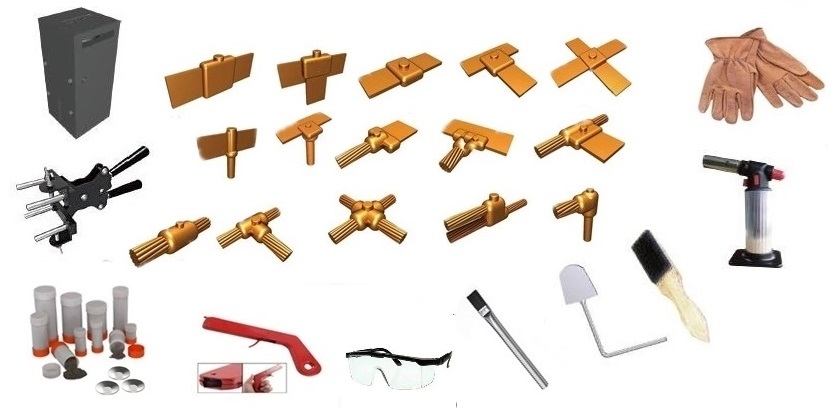
Before the weld begins
Use the mould, charge and accessories specified for the conductor sizes and joint geometry. Missing or substituted components can affect safety and weld quality.
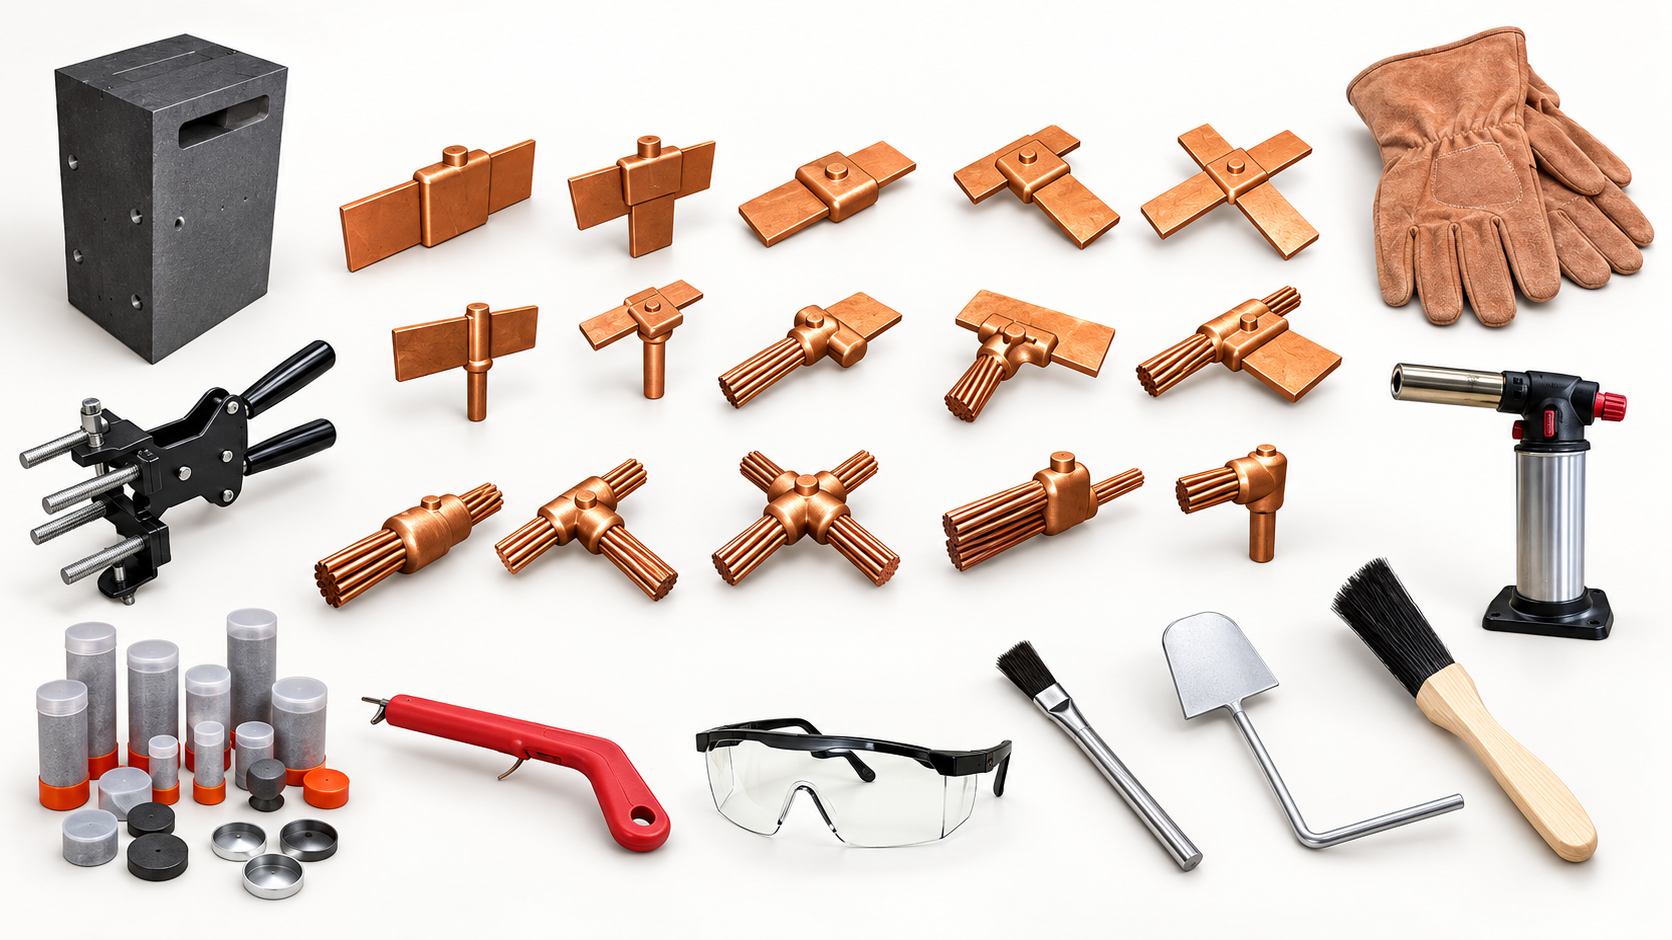
Also required: natural-bristle mould brush, conductor wire brush and the protective equipment specified for the work.
Exothermic welding process
The sequence below follows the supplied field procedure directly. Each step is concise, ordered and paired with the original process imagery where available.
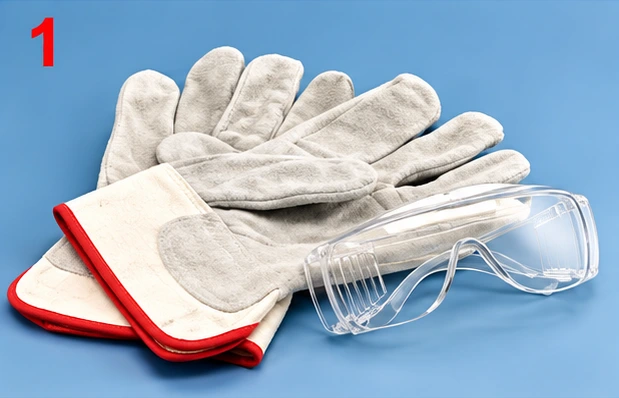
Wear safety glasses and gloves before handling welding products.
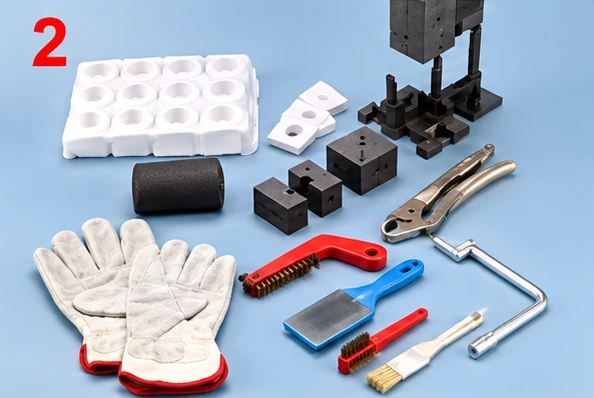
Prepare the mould, clamp, weld material, brushes, igniter and torch. Confirm that the mould is intact.
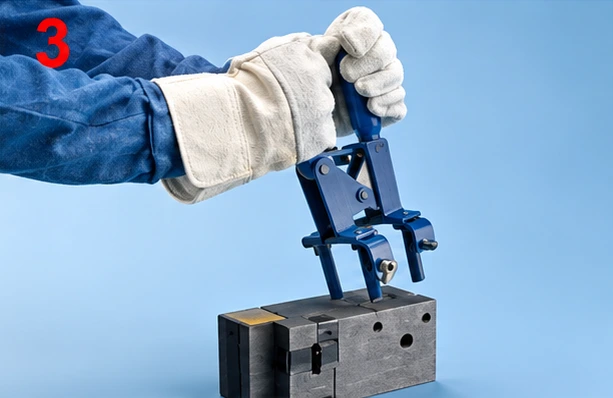
Slide the clamp into the mould holes with the thumbscrews correctly oriented.
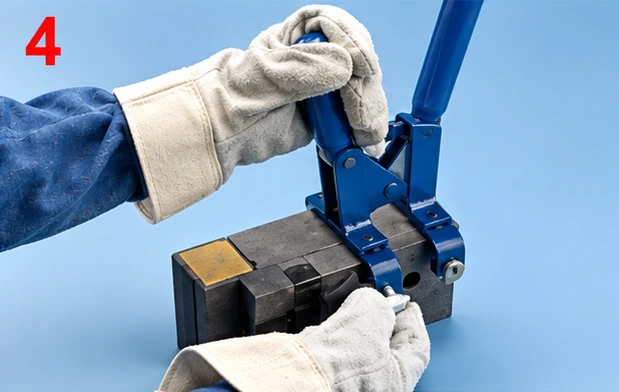
Tighten the clamp thumbscrews firmly onto the mould.
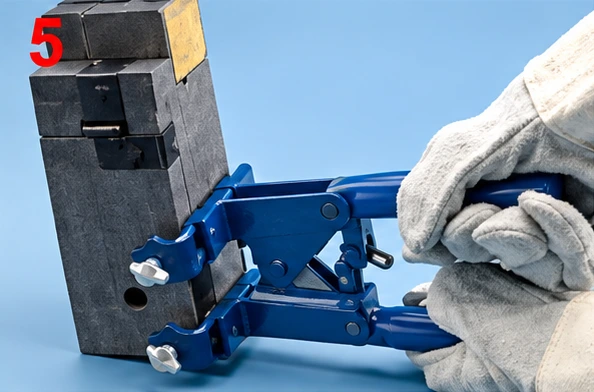
Close the grips and adjust the clamp until both mould halves fit tightly.
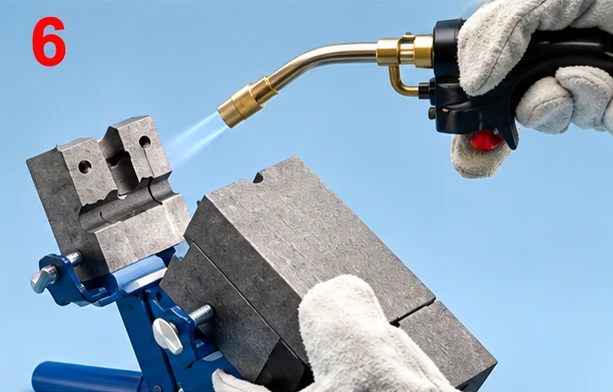
Clean and dry the conductor, then preheat the mould to remove moisture. Reheat only when needed between welds.
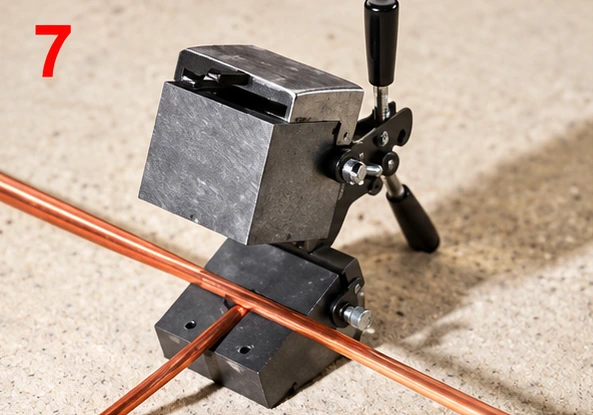
Position the conductors, close the clamp and seal any gap that could cause leakage.
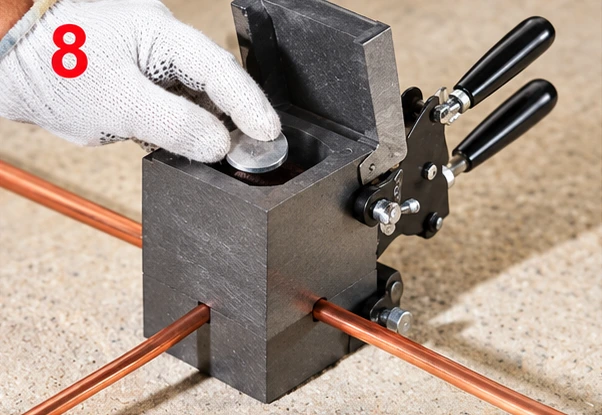
Block the tap hole with the specified metallic disk.
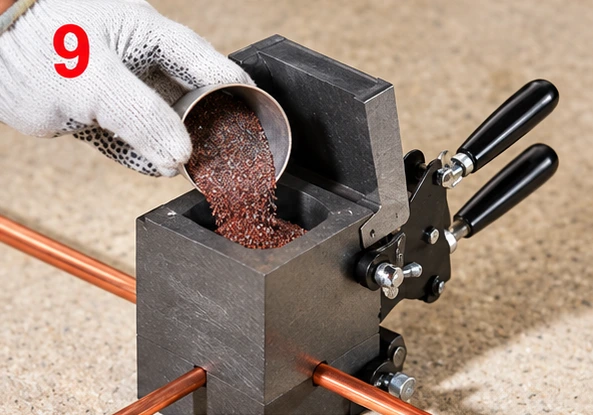
Empty the complete welding-mixture package into the mould crucible.
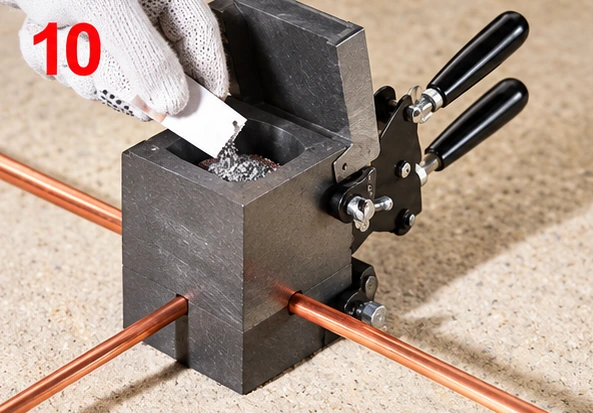
Scatter half over the charge. Close the lid and place the remainder near the ignition opening.
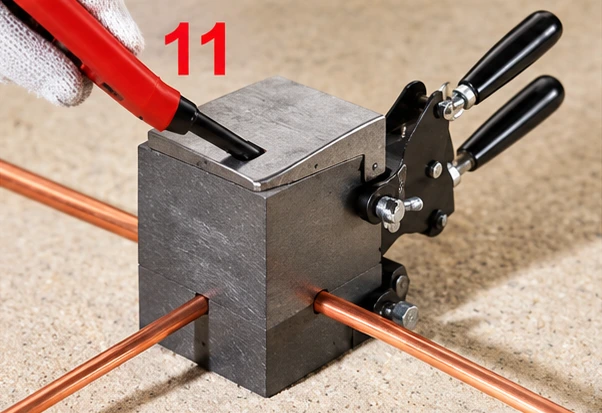
Ignite the starting powder at the top or side using the flint igniter.
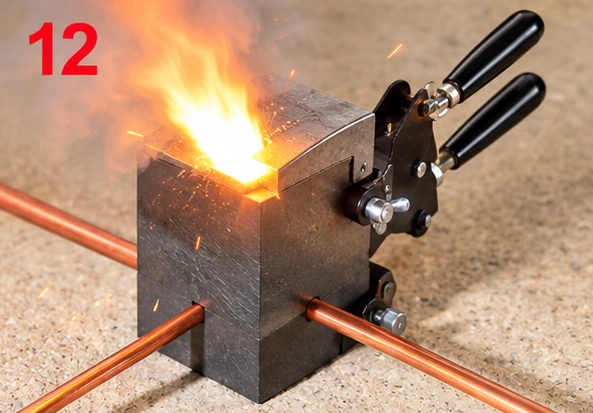
Stand clear while the reaction completes in approximately 3–4 seconds.
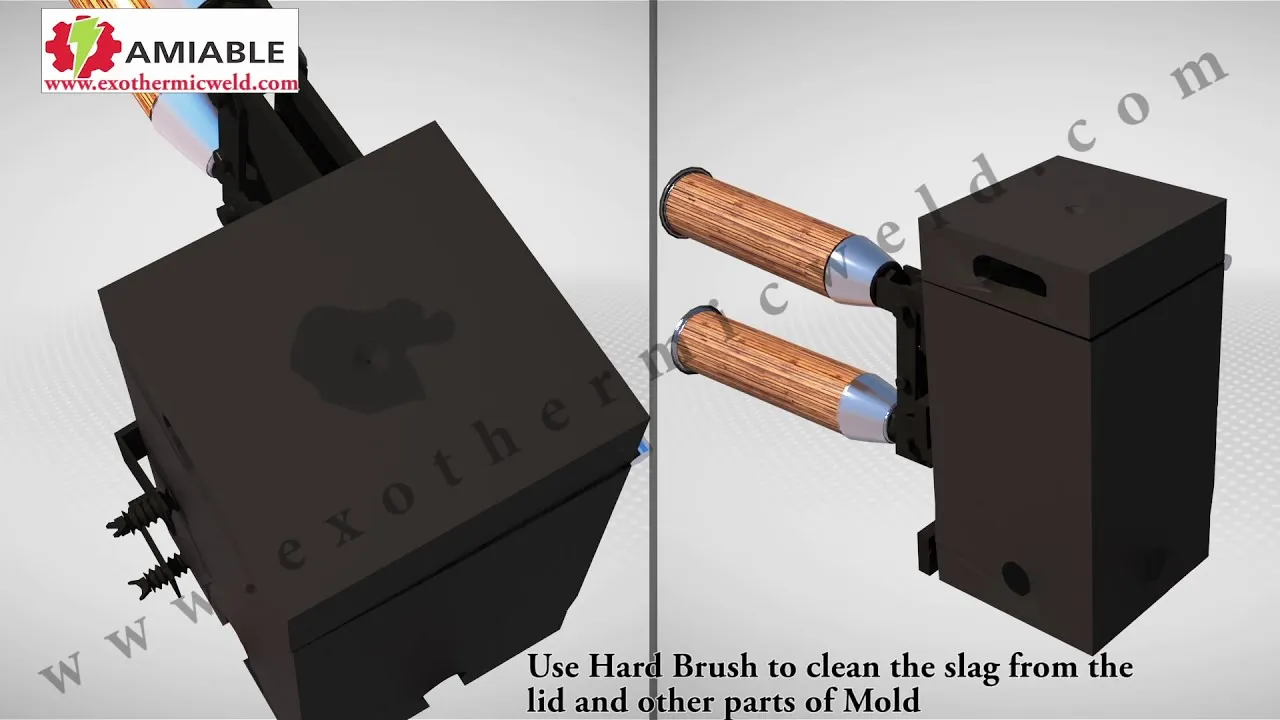
After at least two minutes, release the handle grip and open the mould. Remove the joint, clear the slag and clean the mould cavities. The warm mould is then ready for the next weld.
For continuous operation, keep at least two correctly specified moulds available. One mould can cool and be cleaned while the other is prepared, helping the team maintain a safe, unhurried sequence.
Connection characteristics
Process control matters because it directly influences the electrical, mechanical and environmental performance of the finished connection.
Designed for long-term service in demanding environmental conditions.
Provides a continuous electrical path with minimal connection resistance.
Avoids a pressure-only interface and reduces problems associated with dissimilar-metal connectors.
Creates a molecular bond capable of withstanding substantial stress and strain.
Maintains consistent electrical and mechanical properties over time.
Supports specified joints involving copper cable, tape, brass, stainless steel and copper-coated steel rods.
Produces a robust joint that does not depend on bolts or routine retightening.
Uses purpose-matched moulds, charges and safety procedures for repeatable execution.
Where the process is used
Exothermic welding is selected where long service life, stable conductivity and resistance to loosening are more important than a removable mechanical joint.
Permanent low-resistance joints for earthing grids and electrical grounding networks.
Durable bonds and selected rail-related connections for signalling and electrical continuity.
Grounding and bonding connections for communication infrastructure.
Reliable current paths for lightning-protection and surge-management systems.
Connections used in systems that protect buried pipelines and structures from corrosion.
Specified electrical connections for vehicle and aircraft manufacturing applications.
General & safety instructions
Exothermic welding is efficient when trained personnel use the correct equipment and respect the thermal, chemical and fire risks of the process.
Wear gloves, safety goggles, protective clothing and a face shield where sparks or molten-metal splash may occur.
Keep the area clean, well ventilated and free from flammable materials before opening any weld-metal package.
Keep weld powder and starting powder dry, sealed and protected from heat, moisture and direct sunlight.
Use only approved ignition equipment, close the mould correctly and stand clear during the reaction.
Allow the weld to cool completely, remove slag, inspect the joint and perform conductivity or specified verification tests.
Why use exothermic welding
When the mould, material and field procedure are correctly matched, the resulting joint supports dependable electrical performance with minimal ongoing intervention.
Explore the weld systemThe connection is not dependent on clamping pressure and is designed to remain stable as it ages.
High conductivity helps minimise connection losses in grounding and bonding systems.
No routine retightening is required after a correctly completed weld.
Approved systems can join copper, steel, aluminium and other specified combinations.
The joint is designed to tolerate demanding electrical and environmental conditions without progressive loosening.
Maintenance & storage
Correct cleaning and dry storage help the graphite mould remain dimensionally sound and ready for safe reuse.
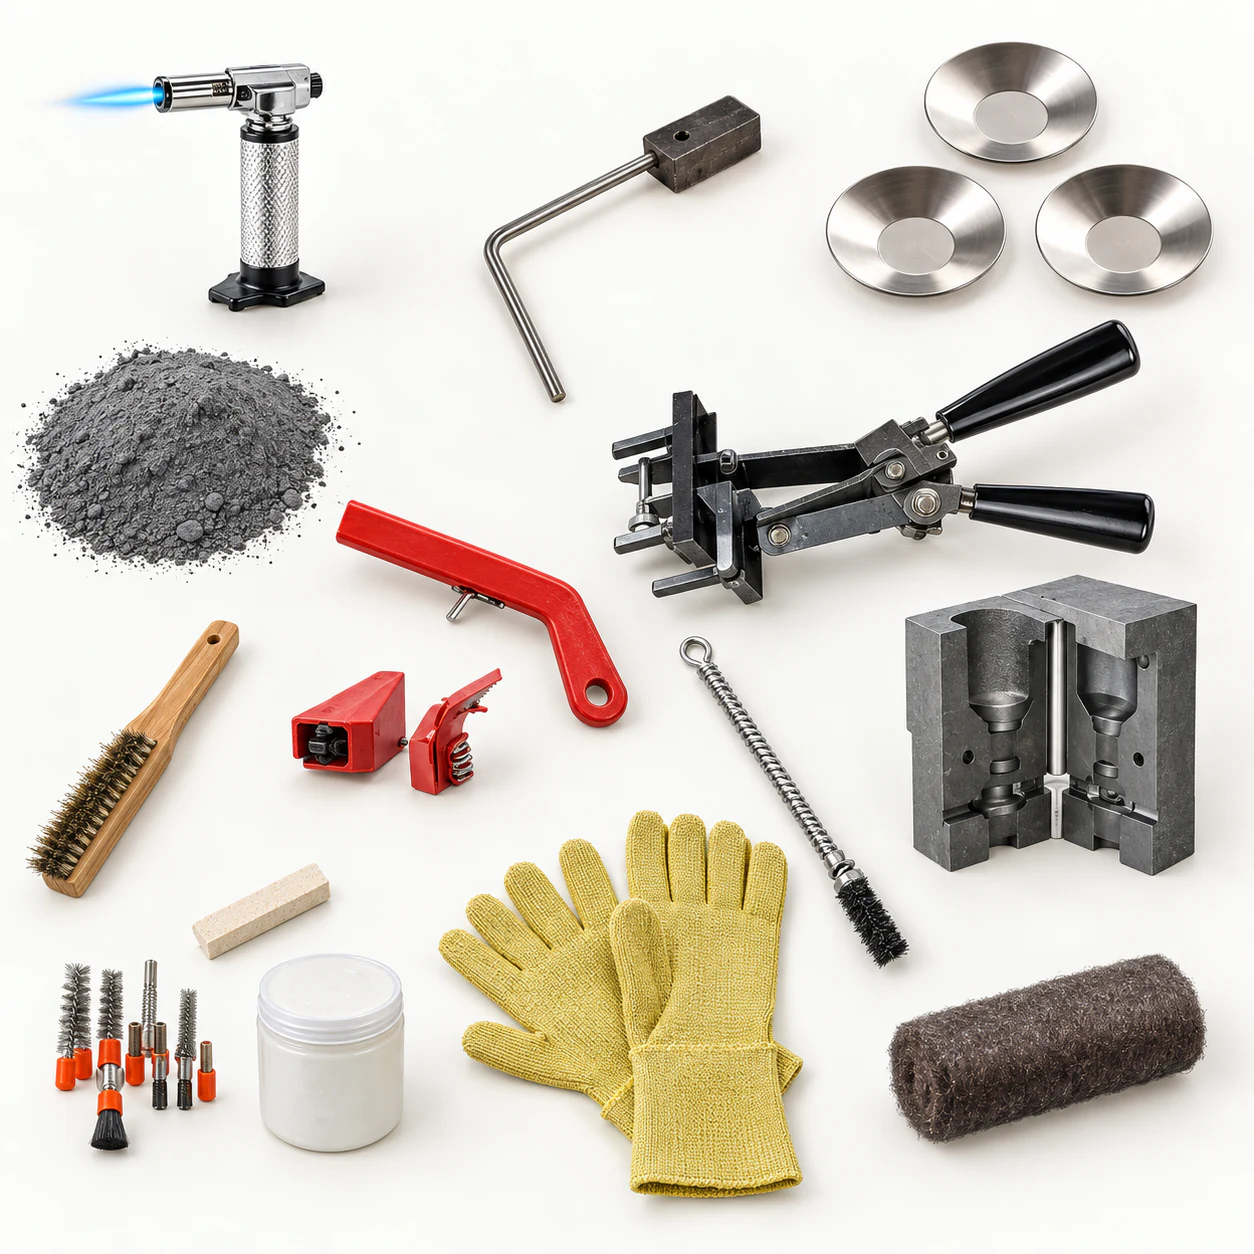
A graphite mould is commonly suitable for approximately 50–60 field connections when it is correctly selected, handled and maintained.
Graphite is fragile. Avoid impact, overtightening and rough tools that can chip the mould or damage the weld cavity.
Let the mould cool sufficiently, then use the specified brush or tool. Do not scrape or clean a hot cavity aggressively.
Clean the mould inside and outside with a soft cloth, clean all accessories and wrap the mould securely in protective bubble packaging.
Store moulds, welding powder and cleaned accessories in a cool, dry location away from direct sunlight and moisture.
Quality & supply support
Amiable Impex supplies exothermic weld powder, graphite moulds and field accessories for projects across India. Orders are coordinated for delivery nationwide, with a typical target window of 10–15 days depending on specification, quantity and destination.
Available quality documentation references CPRI testing, CE and RoHS approvals, together with the company’s stated ISO 9001:2008 quality certification.
Process FAQs
Quick technical guidance covering temperature, cooling time, mould life, moisture control, inspection and storage.
Ask a technical questionExothermic welding is a controlled chemical process that produces molten metal inside a graphite mould. The molten metal surrounds the prepared conductors and solidifies into a permanent molecular connection.
The aluminium and copper-oxide reaction generates temperatures above 1,300°C. Exact reaction behaviour depends on the specified weld material, mould and connection design.
This guide specifies waiting at least two minutes before opening the mould. Always follow the cooling time stated for the selected system and joint configuration.
Moisture can expand rapidly when exposed to molten metal and can compromise both safety and weld quality. Preheating helps remove absorbed moisture before the charge is loaded.
Yes. A mould may typically produce approximately 50–60 field connections when it remains intact and is cleaned and handled correctly. Actual life depends on use and condition.
Inspect the joint for complete fill, a uniform surface, cracks and other visible imperfections. Remove slag and complete electrical or project-specific testing when required.
Keep weld powder and starting powder sealed in a cool, dry environment away from moisture, heat and direct sunlight, following the product safety information.
Plan the connection correctly
Share the conductor materials, sizes, joint type, project quantity and delivery location. Our team can help identify the appropriate exothermic welding system.